Heavyweight Streetwear & Premium Ribbed Knit Collections
CE Certified Ribbed Knit Tops Manufacturing: Technical Quality Architecture & European Compliance
In the hyper-competitive global apparel import landscape, securing a trusted CE certified wholesale ribbed knit tops manufacturer & exporter is no longer merely a procurement preference—it is a critical regulatory imperative for brand protection and market entry into the European Economic Area (EEA). As a Los Angeles-headquartered global apparel manufacturing titan, Urban Nation Apparel bridges the gap between high-fashion silhouette engineering and stringent European textile safety norms. CE certification in knitted apparel validates that garments conform to rigorous health, safety, and environmental protection standards under relevant EU Directives, including EN ISO 13688 (General Requirements for Protective & Commercial Clothing) and strict compliance with REACH Regulation (EC 1907/2006) regarding hazardous substance limits.
Ribbed knit fabrics present unique structural challenges during manufacturing due to their alternating wale and course loop dynamics. Unlike flat jersey knits, ribbed structures (ranging from 1x1 baby rib to 2x2 fine gauge and 3x3 heavy ribbing) possess inherent elastic memory and dimensional tension. Our certified manufacturing facilities employ computerized circular and flat knitting machinery (equipped with German-engineered Groz-Beckert needles) to guarantee consistent needle bed spacing, eliminating wale skewing, spirality, and edge curling.
Every production batch undergoes comprehensive laboratory testing for dimensional stability after domestic laundering (ISO 6330), color fastness to rubbing and perspiration (ISO 105-X12/E04), and bursting strength parameters (ISO 13938-1). By embedding rigorous quality assurance checkpoints at yarn spinning, greige fabric knitting, reactive dyeing, and final cut-and-sew phases, Urban Nation Apparel delivers commercial garments that exceed compliance requirements while maintaining luxurious hand-feel and long-lasting elastomeric recovery.
| Rib Construction Type | Common Yarn Composition | Fabric Weight (GSM) | Elastane / Spandex Ratio | Target Elasticity Recovery | Primary Commercial Application |
|---|---|---|---|---|---|
| 1x1 Micro Rib | 95% Combed Cotton / 5% Elastane | 180 - 220 GSM | 4% - 6% High-Tension | ≥ 96.5% after 50 cycles | Fitted Layering Tops, Base Layers |
| 2x2 Heavy Rib | 100% Organic Ring-Spun Cotton | 280 - 350 GSM | Natural Mechanical Stretch | ≥ 92.0% structural recovery | Streetwear Tank Tops, Mock Neck Tees |
| 3x3 Chunky Rib | 80% Cotton / 20% Recycled Poly | 360 - 450 GSM | Optional 3% Spandex Core | ≥ 94.0% shape retention | Heavyweight Outerwear Tops, Cardigans |
| Variable Needle-Out Rib | Micro-Modal / Nylon / Spandex | 210 - 260 GSM | 7% Micro-Spandex Blend | ≥ 98.0% dynamic stretch | Elevated Designer Bodysuits & Crops |
Advanced Textile Engineering & Customization Technologies
Precision Knitting & Gauge Density
Utilizing 12G, 14G, and 16G Stoll computerized knitting systems, we control needle-bed tension to prevent dimensional distortion, ensuring consistent course-to-wale ratios across high-volume production orders.
Specialty Garment Wash Processes
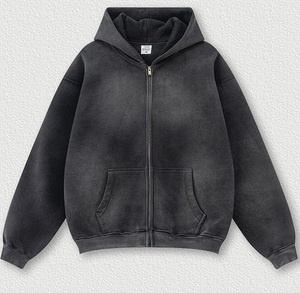
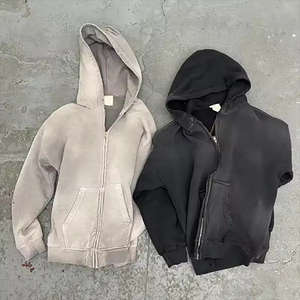
From vintage acid washes and sun-faded pigment dyes to enzyme stone washes and silicone softening, our wash tech delivers unique aesthetics without compromising structural tensile integrity.
3D Puff & Screen Printing Integrity
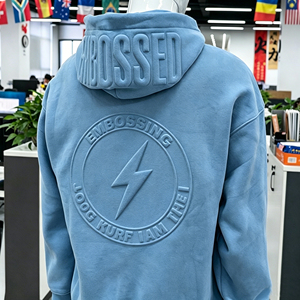
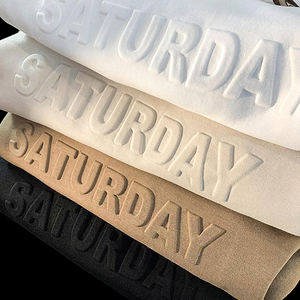
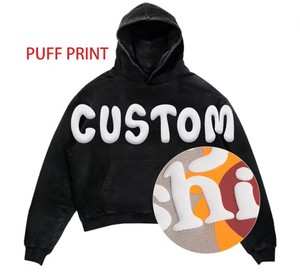
Advanced high-density silicone inks and 3D puff print formulations engineered specifically to adhere to high-stretch ribbed surfaces without cracking, peeling, or color bleeding.
Future Procurement Trends in Wholesale Ribbed Knit Top Manufacturing
As global retail buyers and private label apparel brands navigate macroeconomic shifts and evolving consumer demands, the procurement strategy for ribbed knit tops is undergoing a fundamental transformation. Procurement directors are migrating away from legacy transactional purchasing toward strategic, technology-integrated manufacturing partnerships. Key trends dominating the 2026–2030 sourcing horizon include:
1. Eco-Conscious Fiber Synthesizing & Circular Fabrics: Brands are demanding GRS (Global Recycled Standard) certified yarns, combining organic BCI cotton with closed-loop recycled elastane (Roica V550) and bio-based lyocell. Sustainable reactive dyes with zero liquid discharge (ZLD) processing are rapidly becoming baseline requirements for CE and EU market compliance.
2. Nearshoring & Dual-Sourcing Multi-Hub Models: To mitigate geopolitical supply chain friction and ocean freight bottlenecks, lead procurement teams utilize Urban Nation Apparel’s multi-region footprint. Fast-turn sampling and short-run production are handled at our Los Angeles and Mexico facilities, while high-volume cost-optimized bulk runs are executed across Vietnam, Bangladesh, and China.
3. Digital Twin Prototyping & 3D Tech Packs: Traditional physical sample iterations add weeks to lead times. We leverage 3D CLO and Browzwear software to simulate ribbed fabric drape, gauge stretch, and seam tension virtually, reducing pre-production approval timelines from 21 days down to 48 hours.
Product Development & Aesthetic Evolution of Ribbed Knitwear
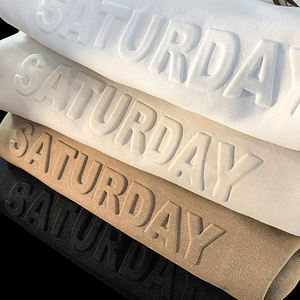
Once considered basic thermal undergarments, ribbed knit tops have evolved into core fashion statements across streetwear, contemporary womenswear, and premium athleisure sectors. Modern garment architecture favors heavyweight GSM constructions (280 GSM to 450 GSM) that offer sculpted compression without sacrificing mobility.
Design innovation is currently focused on hybrid distress treatments—combining vintage sun-faded wash techniques with targeted acid washing to impart an authentic worn-in aesthetic. Seamless 3D knitting technology is also gaining rapid market share, eliminating side seams entirely for sleek body-con silhouettes that enhance comfort and reduce fabric cutting waste by up to 18%. Furthermore, drop-shoulder cropped fits and raw-edge hems backed by stay-stitching represent major growth segments in private label streetwear production.
Urban Nation Apparel: Vertically Integrated Global Apparel Powerhouse
Headquartered in Los Angeles, California, Urban Nation Apparel (DAR Fashions) operates as a fully vertically integrated design and manufacturing enterprise. We bridge the gap between creative fashion concepts and large-scale industrial garment production for global brands.
Global Production Network: Our state-of-the-art manufacturing facilities span China, Bangladesh, Vietnam, and Mexico, giving buyers flexible sourcing strategies, competitive FOB/CIF tariffs, and rapid turnaround schedules tailored to order scale.
End-to-End OEM/ODM Expertise: Specializing in womenswear, menswear, streetwear, and elevated fashion basics, we manage every phase of the value chain—yarn procurement, knit pattern engineering, custom garment washing, 3D puff printing, custom labelling, and final export logistics.
Frequently Asked Questions (FAQ) for B2B Sourcing
Request Full Product Catalog & B2B Wholesale Pricing
Connect directly with our Los Angeles design engineering team and global production specialists to receive complete tech packs, sample kits, and volume price breaks.