Strategic B2B Sourcing from a World-Class Floral Print T Shirt Factory
In the rapidly evolving global fashion ecosystem, sourcing from a reliable Floral Print T Shirt Factory requires much more than simply matching sample swatches. Modern fashion houses, direct-to-consumer (D2C) unicorns, and corporate retail buyers need an OEM/ODM manufacturing partner capable of translating intricate botanical artwork into durable, high-margin, commercially viable garments. As consumer demand shifts toward nuanced digital prints, sustainable bio-based inks, and vintage distressed garment washes, procurement executives are challenged to balance premium visual aesthetics with strict cost-per-unit targets and rapid speed-to-market.
At Urban Nation Apparel, headquartered in Los Angeles, California with overseas manufacturing infrastructure spanning China, Vietnam, Bangladesh, and Mexico, we solve the core structural challenges of print execution, fabric shrinkage, wash fastness, and tariff optimization. Whether your brand requires high-resolution Direct-to-Garment (DTG) printing for micro-run capsules or large-scale Rotary Screen All-Over Print (AOP) production for mass retail distribution, our engineering team ensures millimeter-precise registration and hand-feel consistency across millions of units.
Print Technologies
Rotary Screen AOP, High-Density Flatbed Screen Printing, Sublimation on Technical Poly-Blends, Digital Pigment DTG, Discharge Printing for Soft Hand-Feel.
Fabric Substrates
100% Combed Ring-Spun Cotton (160-240 GSM), Organic GOTS Cotton, Modal-Cotton Blends, Recycled Polyester (rPET), Bamboo Viscose, Slub & French Terry Knits.
Specialty Garment Finishing
Enzyme Stone Wash, Mineral Wash, Acid Wash, Sun-Faded Vintage Tinting, Silicone Softener Treatment, Anti-Pilling Bio-Polishing.
Quality Assurance & Compliance
AQL 2.5/4.0 Inspection Standards, OEKO-TEX Standard 100 Certified Inks, WRAP & SMETA Audited Facilities, ISO 9001 Production Management.
Factory Recommended Floral Print T-Shirt Lines for Global Procurement
Navigating seasonal collections requires a tailored approach to silhouette selection, pattern scale, and fabric weight. Below are our top factory-recommended floral print t-shirt categories engineered for maximum market penetration, high shelf appeal, and superior gross margins for wholesale distributors and fashion labels.
Featured Production Showcase
Each silhouette shown below reflects our mastery in cut-and-sew garment construction, specialized dye house treatments, and high-fidelity print application.
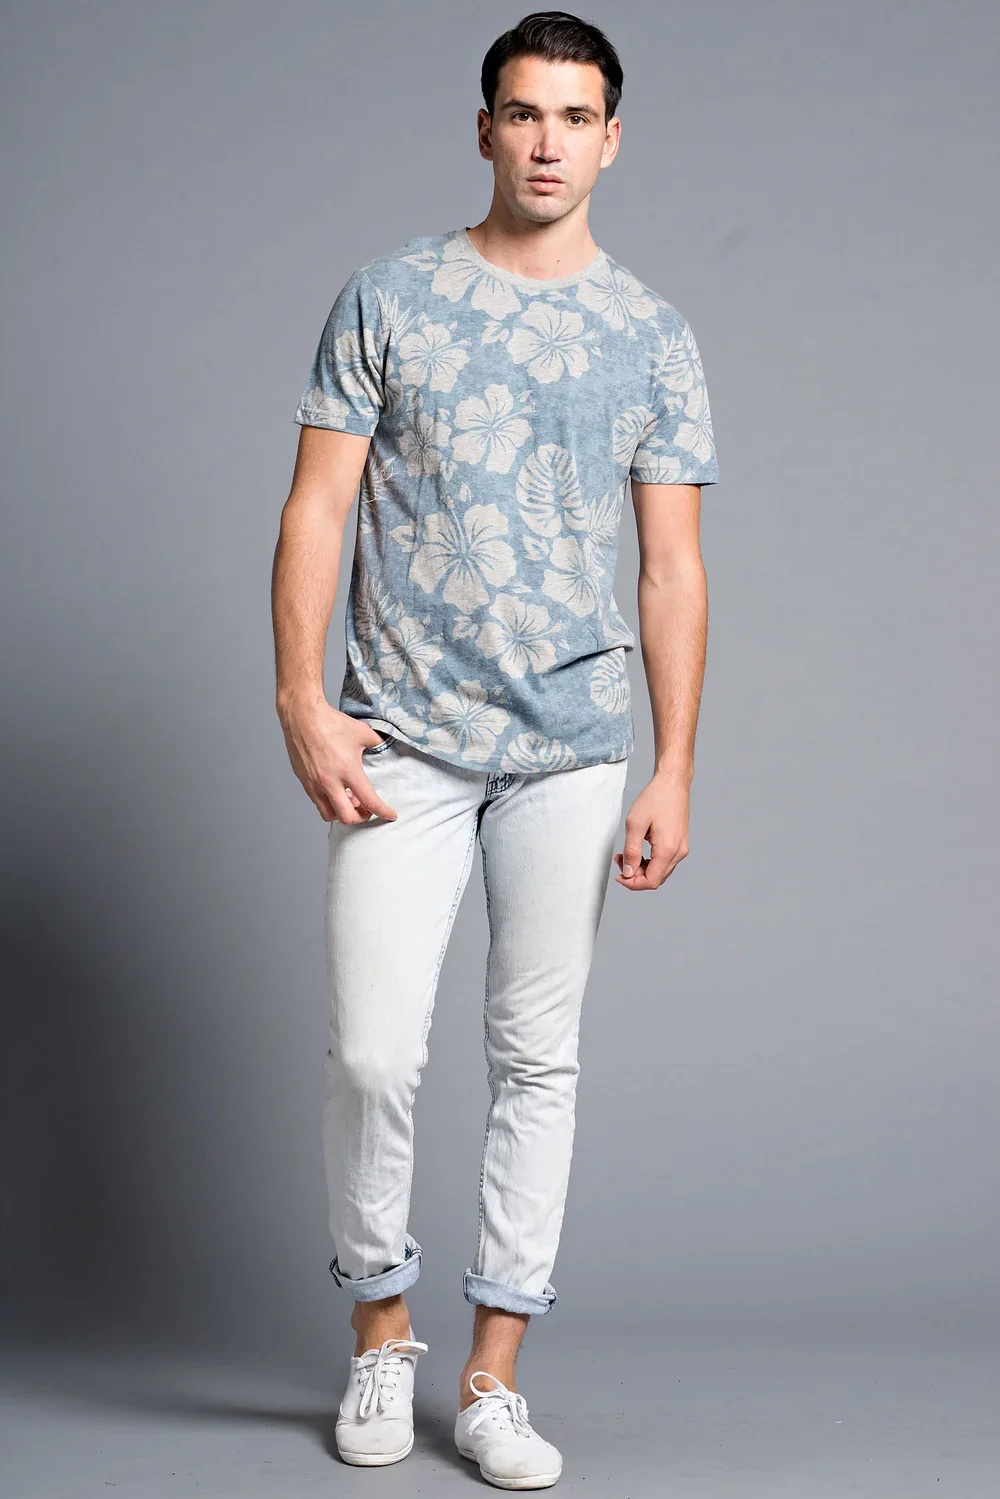
Light Blue Botanical Floral Tee
Fabric: 180 GSM 100% Combed Cotton
Print Method: Water-based Screen Print / Soft-touch Pigment
Ideal For: Resort Wear, Spring/Summer Menswear Capsules
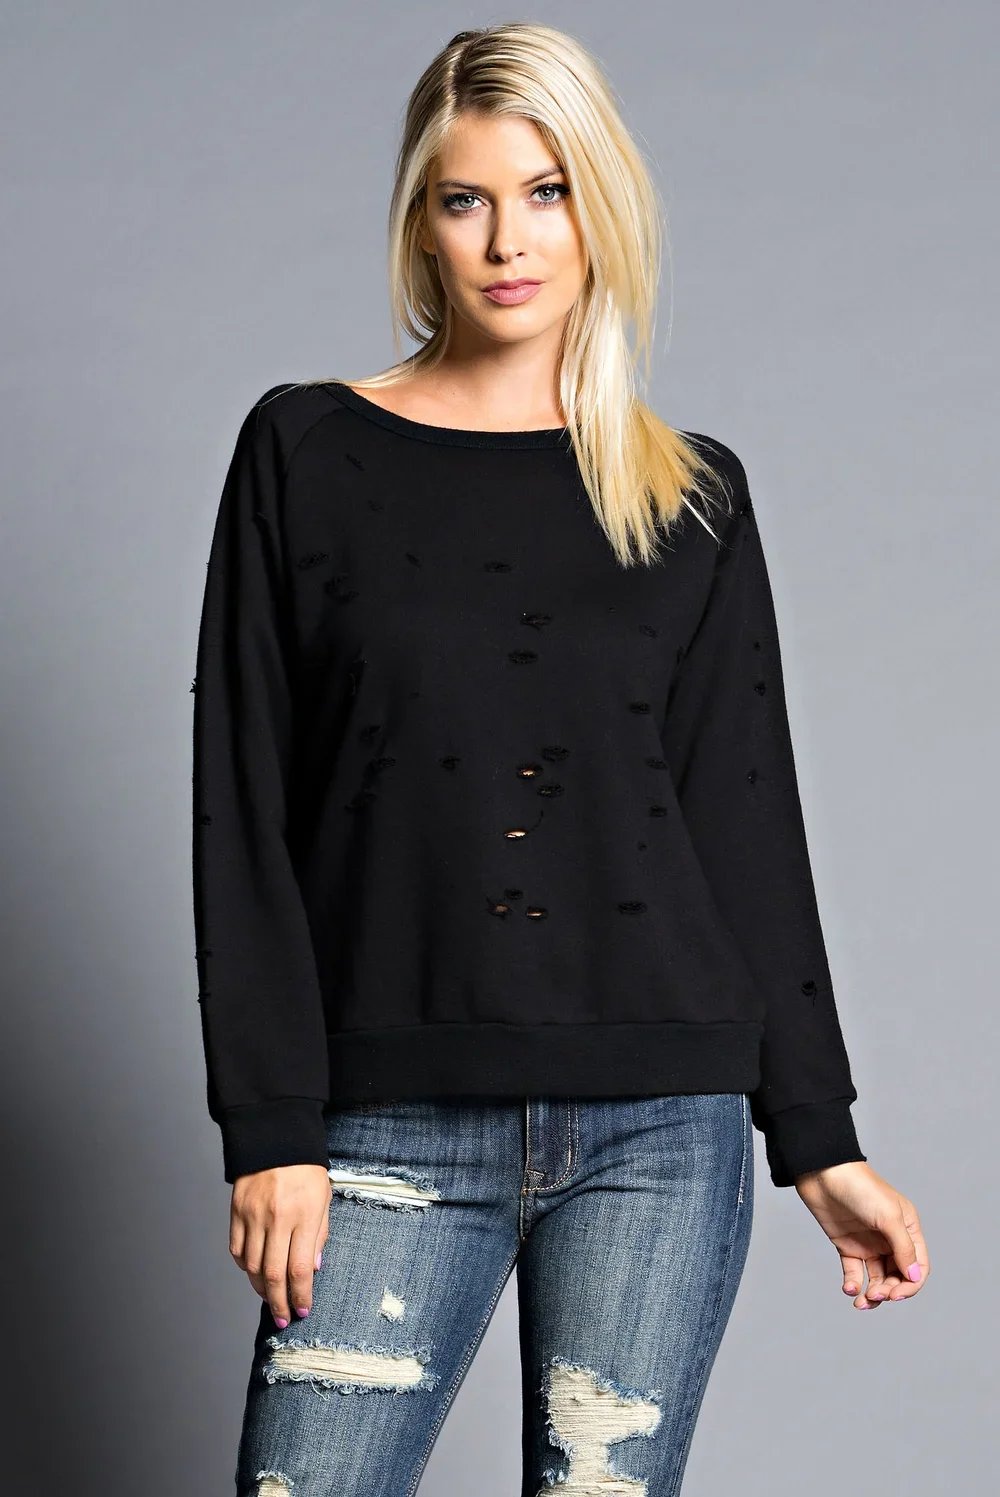
Vintage Acid-Washed Print Tee
Fabric: 220 GSM Heavyweight Cotton Slub
Process: Specialty Enzyme Wash + Distressed Printing
Ideal For: Streetwear Brands, Contemporary Urban Collections
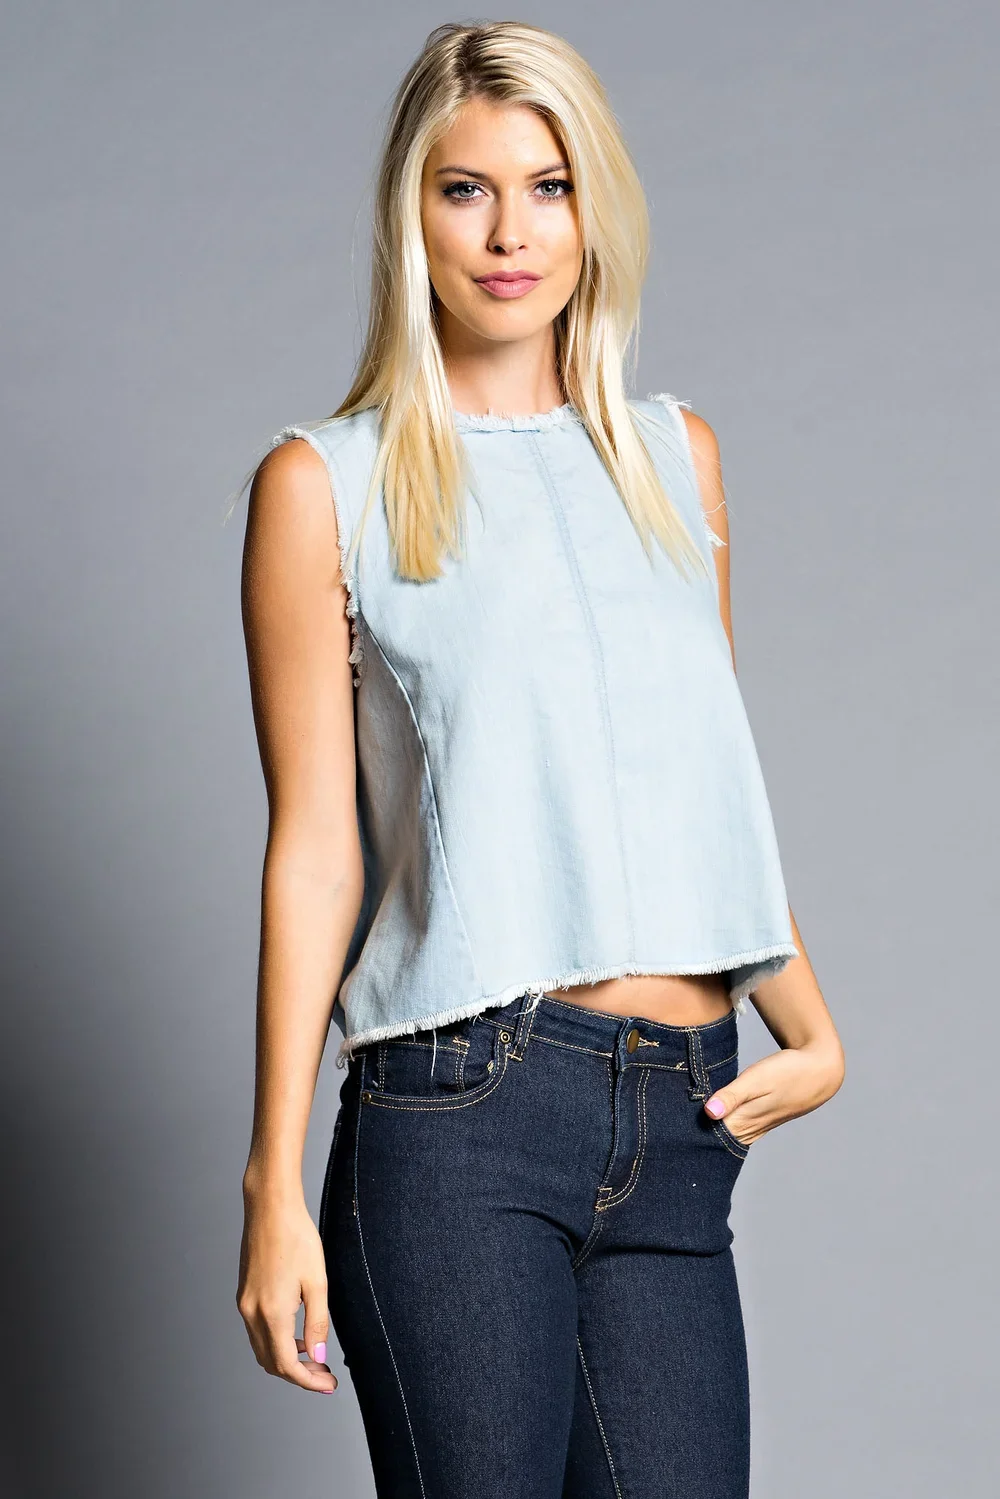
Resort Casual Cut-and-Sew Top
Fabric: Cotton-Linen / Rayon Blend
Process: All-Over Rotary Print + Enzyme Softening
Ideal For: Premium Casual Brands & Cruise Collections
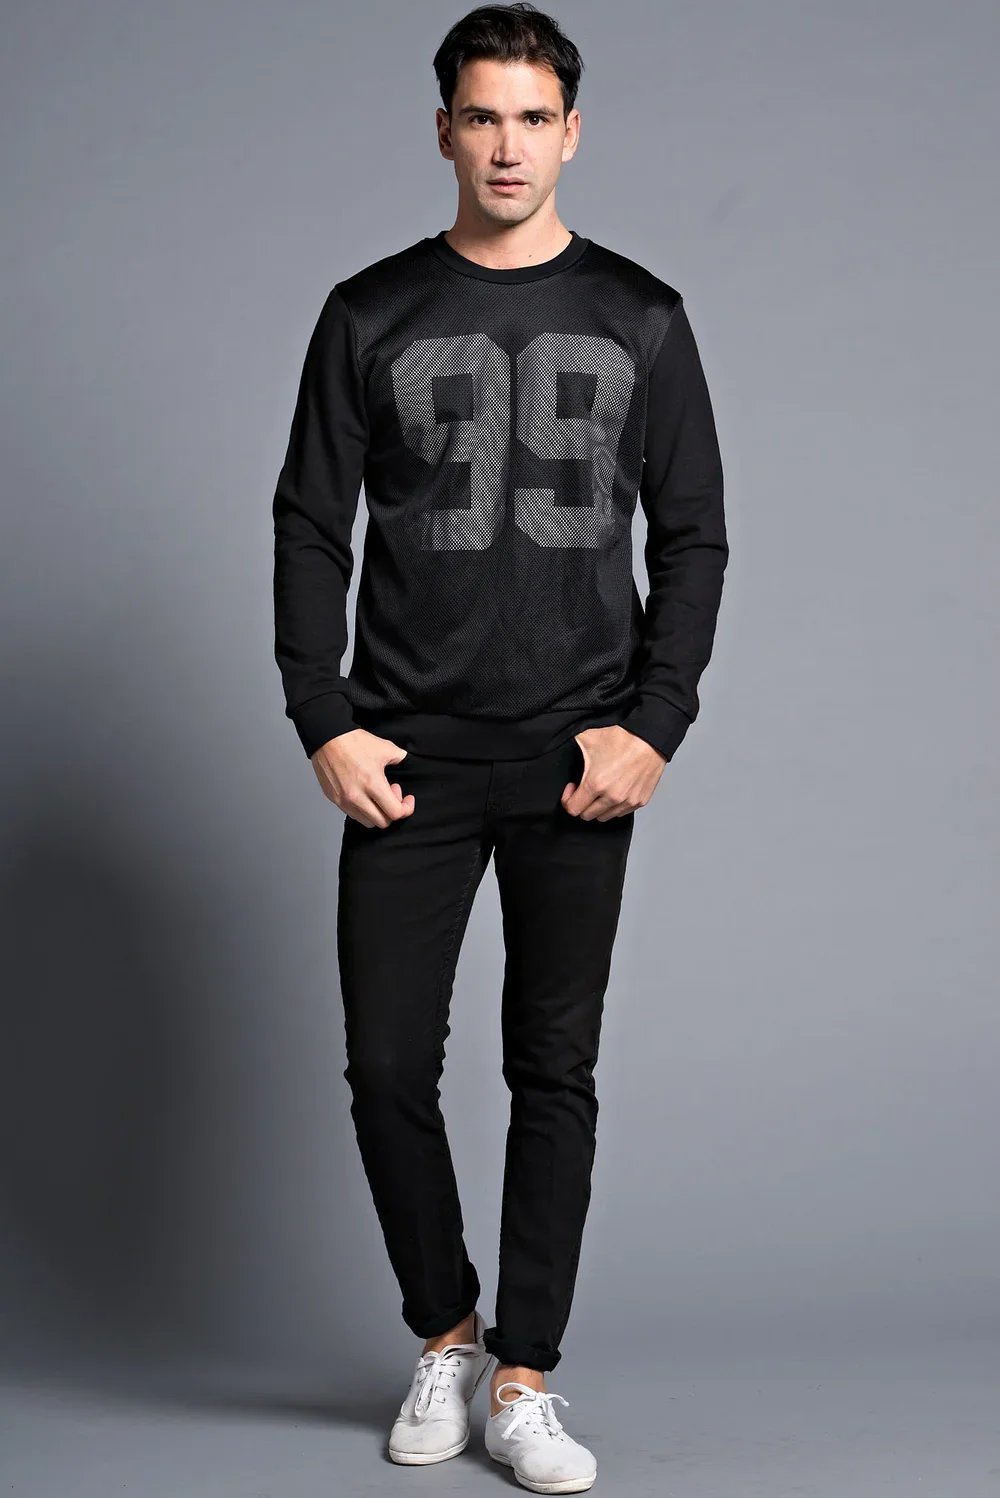
Oversized Heavyweight Statement Tee
Fabric: 240 GSM Carded Open-End Cotton
Process: High-Density Screen Print & Placement Graphic
Ideal For: Youth Culture & Trend-Driven Streetwear
1. Tropical & Hawaiian All-Over Print (AOP) T-Shirts
Engineered using continuous rotary screen printing or high-speed digital roll-to-roll printing before panel cutting, our tropical floral tees offer full seam-to-sew coverage without print cracking at armhole or neckband junctions. Utilizing 160-180 GSM combed ring-spun cotton or Modal blends, these shirts feature vibrant hibiscus, palm leaf, and paradise botanical motifs with exceptional color fastness (Grade 4+ under ISO 105-C06 standards).
2. Vintage & Sun-Faded Distressed Floral Tees
Combining garment-dyeing techniques with placement screen printing, our vintage floral series replicates authentic 1990s archival aesthetics. We apply reactive dyes, followed by custom enzyme stone washing, ozone distressing, and micro-abrasion along rib collars and hem edges. The print utilizes discharge inks that bleed seamlessly into the fabric fiber rather than sitting heavily on top, yielding an ultra-soft hand feel desired by high-end boutique brands.
3. Minimalist Micro-Floral & Botanical Embroidery Blends
For refined, subtle menswear and womenswear collections, our factory produces micro-floral repeat prints (ditsy patterns) matched with intricate high-density chest embroidery. Our multi-head Tajima embroidery machinery works in tandem with screen printing tables, allowing brands to combine tactile 3D thread work with delicate botanical prints in a single seamless production line.
4. Eco-Friendly Organic & Recycled Floral Performance Tees
Targeted at conscious consumers and outdoor activewear lines, these tees incorporate 50% GOTS-certified organic cotton blended with 50% Recycled Poly (rPET) derived from post-consumer plastic bottles. Printed exclusively using water-based, GOTS-approved inks free from phthalates, PVC, and heavy metals, these products comply with North American and European eco-legislation without compromising color vibrancy or stretch recovery.
Future Global Procurement Trends in Floral Print T-Shirt Manufacturing
As global supply chains navigate macroeconomic shifts, AI-driven demand forecasting, and tightening environmental regulations, apparel procurement heads must align with factories that embody future-proof manufacturing capabilities. Sourcing floral printed garments over the next decade will be defined by five major structural shifts:
A. Multi-Country Dual-Shoring & Nearshoring Agility
Relying on a single manufacturing origin presents immense trade risks. Modern procurement strategy favors a hybrid model: leveraging high-capacity Asian hubs (China, Vietnam, Bangladesh) for cost-efficient, high-volume seasonal core runs, alongside nearshore facilities in Mexico for rapid 3-week turnaround replenishment orders. Urban Nation’s dual-headquarters approach (Los Angeles design & logistics + multi-regional international factories) allows brands to dynamically shift production based on tariff fluctuations, shipping container availability, and peak demand spikes.
B. Shift from Plastisol to Water-Based & Bio-Pigment Inks
Regulatory authorities such as the EU REACH framework and the US Consumer Product Safety Improvement Act (CPSIA) are aggressively restricting traditional plastisol formulations containing petroleum solvents and phthalates. Future-focused floral print factories are investing in zero-liquid-discharge (ZLD) digital pigment printing systems and algae-based inks that reduce water consumption by up to 85% during the wash cycle while eliminating hazardous chemical runoff.
C. Micro-Capsules and On-Demand Batch Sourcing
The traditional 6-month seasonal production cycle is increasingly replaced by agile 30-to-45-day micro-capsules driven by social media trending algorithms. To prevent inventory write-offs, buyers demand flexible Minimum Order Quantities (MOQs) starting as low as 300 to 500 pieces per style/colorway. Advanced direct-to-fabric digital printing enables factories to run multiple floral colorways on a unified master fabric roll, lowering setup costs and eliminating expensive screen engraving fees for small runs.
D. Traceability & Digital Product Passports (DPP)
European Union directives mandating Digital Product Passports (DPP) by 2026 require complete transparency from raw cotton fiber origin to final garment finishing. Leading floral print t-shirt suppliers are integrating RFID micro-chips and QR-coded care labels that allow end consumers and customs inspectors to verify organic certifications (GOTS), OEKO-TEX eco-friendly ink credentials, and fair-labor factory audit reports in real time.
E. AI-Assisted Color Matching & Automated Defect Scanning
Color consistency between sample approvals (lab dips) and bulk production has historically been a friction point in printed textiles. Modern manufacturing facilities deploy spectrophotometers linked to automated dye-dispensing software, ensuring shade matching within Delta E < 0.8 tolerance. Furthermore, inline optical camera scanners inspect printed fabric webs at 60 meters per minute, automatically flagging misregistrations, ink splatters, or thread flaws before panel cutting occurs.
Product Development & Design Innovation Trends for Printed Apparel
Designing high-selling floral printed t-shirts requires deep synchronization between fashion forward aesthetics and factory-level print feasibility. Below are the prominent design innovation trends defining current and upcoming retail seasons:
1. Gothic & Dark Botanical Realism
Moving away from pastels, current streetwear favors dark background floral prints—incorporating moody roses, wilted flora, and baroque botanical illustrations printed on jet-black, charcoal, or deep navy heavyweight combed cotton.
2. Mixed Media: Print + Puff + Rhinestone
Multi-dimensional embellishments are surging in popularity. Factories apply soft-base floral prints overlaid with raised 3D puff screen print accents, foil highlights, or hot-fix rhinestones to create elevated tactile textures.
3. Gender-Neutral Oversized Cut-and-Sew
Modern floral t-shirts feature dropped shoulders, wider sleeve openings, and boxy, relaxed silhouettes (220-260 GSM). The design appeals across gender demographics, allowing brands to streamline SKU counts.
4. Photo-Realistic Botanical Sublimation
Utilizing high-DPI digital heat transfer printing on specialized poly-cotton or tri-blend fabrics, designers capture intricate photographic floral artwork with lifelike depth, gradient shading, and infinite color palettes.
Comprehensive B2B Sourcing FAQ: Frequently Asked Procurement Questions
Below are detailed, engineer-backed answers to the most common technical and operational questions posed by global sourcing managers, fashion directors, and supply chain executives when evaluating a Floral Print T Shirt Factory.
Q1: What is the minimum order quantity (MOQ) for custom floral print t-shirts?
Answer: Our flexible OEM/ODM manufacturing model accommodates varying brand scales. For standard screen-printed or placement graphic floral tees, our baseline MOQ starts at 300 pieces per style/colorway across standard size runs (S-XXL). For complex All-Over Print (AOP) rotary screen orders or custom reactive garment-dyed collections, the MOQ typically ranges between 500 to 1,000 pieces depending on fabric knit customization and pattern repeat complexity. Small-batch digital DTG sampling and micro-capsule runs are also available for qualified brand partners.
Q2: Which printing method is best for floral print t-shirts: Screen Printing, DTG, or Sublimation?
Answer: The ideal print process depends directly on fabric composition, artwork complexity, order volume, and desired hand feel:
• Water-Based Screen Printing: Best for high-volume 100% cotton orders (500+ units) requiring extremely soft hand feel, high color vibrancy, and long-term wash durability.
• Direct-to-Garment (DTG): Best for complex, multi-color photographic floral art with fine gradients on 100% cotton, especially for small batch orders or print-on-demand replenishment.
• Sublimation Printing: Ideal for 100% polyester or high-poly technical fabric blends where all-over seam-to-sew floral coverage is required without compromising fabric breathability or fading.
• Discharge Printing: Ideal for dark-colored 100% cotton garments where the dye is chemically removed and replaced with floral pigments, yielding zero added weight or stiffness on the shirt.
Q3: How does the factory ensure color accuracy and prevent pattern bleeding after washing?
Answer: Color precision is managed using standardized Pantone Matching System (PMS) TCX/TPG color codes calibrated via digital spectrophotometers (Delta E < 0.8). To completely eliminate post-consumer dye migration or print fading, all printed fabrics undergo pre-shrunk steam processing, high-temperature heat-curing (160°C for 3 minutes for water-based inks), and rigorous post-wash testing under ISO 105 and AATCC standards for color fastness against rubbing (crocking), laundering, and perspiration.
Q4: What is the standard sample development and bulk production turnaround time?
Answer: Our streamlined product development pipeline operates under the following timelines:
• Tech Pack & Artwork Review: 24–48 hours.
• Sample & Lab Dip Creation: 7–12 business days (includes custom fabric knit, dye, strike-off print, and express air courier to your office).
• Bulk Production Lead Time: 25–35 calendar days upon PP (Pre-Production) sample approval. Express production slots (18–21 days) are available via our nearshore Mexico production facility for urgent retail launch windows.
Q5: Can Urban Nation Apparel handle custom tech packs, custom neck labeling, and retail-ready packaging?
Answer: Yes, we provide full white-label and private-label turn-key manufacturing. Our services include technical spec-sheet creation, custom woven or heat-seal screen-printed neck labels, custom hangtags, barcode sticker application, individual eco-friendly polybagging, and master carton packing compliant with Amazon FBA, Nordstrom, or Target EDI distribution center requirements.
Q6: How do you handle shipping, customs clearance, and import duties for international clients?
Answer: We offer comprehensive global logistics capabilities including FOB, CIF, DDP (Delivered Duty Paid), and LDP (Landed Duty Paid) terms. Our logistics team handles export documentation, customs clearance, duty payment, and door-to-door freight forwarding to warehouses across North America, Europe, Australia, and the Middle East, taking the operational burden entirely off your procurement team.
Q7: What quality control protocols are implemented during bulk floral print production?
Answer: Quality assurance is integrated into every stage of production under strict ISO 9001 and AQL (Acceptable Quality Limit) 2.5 standard criteria. We perform:
1. Raw Material Inspection: 4-point fabric inspection system prior to cutting.
2. In-Line Inspection: Continuous optical monitoring during print application and seam stitching.
3. End-Line Finishing Inspection: 100% visual inspection for loose threads, print alignment, measurement tolerances (+/- 1cm), and stain checks.
4. Final Pre-Shipment Inspection: Random sampling audit before carton sealing with detailed inspection reports delivered to the client.
Why Urban Nation Apparel Is the Strategic Manufacturing Partner Choice
Headquartered in the fashion hub of Los Angeles, California, Urban Nation Apparel stands as a premier vertically integrated design and manufacturing powerhouse. We bridge the gap between western fashion sensibility and global high-volume manufacturing efficiency.
Vertically Integrated Operations
From yarn spinning, fabric knitting, and custom dye bath formulation to automated cutting, advanced printing, and precision sewing, we control the complete manufacturing value chain to deliver uncompromised quality.
Multi-National Production Network
Strategically operating state-of-the-art facilities across USA (Los Angeles), China, Vietnam, Bangladesh, and Mexico, giving clients unmatched flexibility in cost optimization, tariff relief, and duty-free trade advantages.
Specialty Garment Finishing Mastery
Industry-renowned expertise in specialty garment wash processing, distressed treatments, sun-bleached finishes, vintage pigment washing, and custom fabric softening that elevate basic tees into premium fashion pieces.
Ethical & Certified Compliance
Committed to worker welfare and sustainability. All partner facilities maintain WRAP, SMETA (SEDEX), OEKO-TEX, and GOTS certifications, guaranteeing fair wages, safe working environments, and non-toxic production practices.
Technical Guide to Fabric Selection for Printed T-Shirts
The success of any printed garment line depends fundamentally on choosing the correct fabric construction. A common mistake made by apparel buyers is selecting heavy artwork for lightweight fabrics, resulting in garment sag, collar distortion, or print puckering. Below is our engineering matrix for pairing floral print styles with appropriate knitted substrates:
- 100% Combed Ring-Spun Cotton (180–220 GSM): The industry gold standard for casual fashion t-shirts. Long-staple cotton fibers are spun to remove impurities, creating a smooth surface that ensures crisp screen print ink adhesion and vibrant color payoff with zero surface fuzz.
- Cotton / Rayon / Polyester Tri-Blends (140–160 GSM): Extremely soft, lightweight, and drapeable. Excellent for feminine floral fashion tees and vintage heathered aesthetics. Works best with soft-water pigment inks or sublimation prints.
- Heavyweight Open-End Cotton (240–280 GSM): Formulated specifically for streetwear brands seeking a boxy, structured silhouette. Handles heavy high-density screen prints, puff embroidery, and all-over dark botanical motifs without fabric deformation.
- Organic Cotton & Modal Blends (160–190 GSM): Delivers a silky, luxurious hand feel with natural moisture-wicking properties. Ideal for eco-conscious luxury brands focus on sustainable loungewear and premium resort collections.
Streamlined 5-Step Order Execution Process
We make global apparel sourcing simple, transparent, and predictable. When you partner with Urban Nation Apparel for your floral print t-shirt manufacturing, your project moves through a disciplined 5-phase quality gate system:
- Phase 1: Concept & Tech Pack Consultation: Our Los Angeles design engineering team reviews your artwork files (AI/PSD/PDF), color specs (Pantone PMS), garment measurements, and target unit costs to determine optimal print technique and fabric construction.
- Phase 2: Sampling & Strike-Off Approval: We produce physical fabric strike-offs (print tests) and fully sewn Pre-Production (PP) samples for fit, color, and wash testing. Samples are delivered worldwide via express courier within 7 to 12 days.
- Phase 3: Bulk Fabric Knitting & Printing: Upon sample sign-off, bulk fabric is knitted, dyed in certified dye houses, and passed through automated printing beds with continuous color spectrophotometer monitoring.
- Phase 4: Cut & Sew, Garment Wash & QC: Printed panels are precision cut using CAD automated cutters, assembled by expert seamstresses, treated with requested wash finishes, and subjected to 100% AQL 2.5 inline quality inspections.
- Phase 5: Custom Packaging & Global Delivery: Garments are custom labeled, hang-tagged, polybagged, boxed in heavy-duty shipping cartons, and dispatched via sea, air, or express freight under your preferred Incoterms (DDP, FOB, LDP).
Whether you are launching a new seasonal floral capsule or expanding a multi-million-piece global retail inventory, Urban Nation Apparel provides the technical depth, manufacturing scale, and creative craftsmanship necessary to dominate the fashion marketplace.